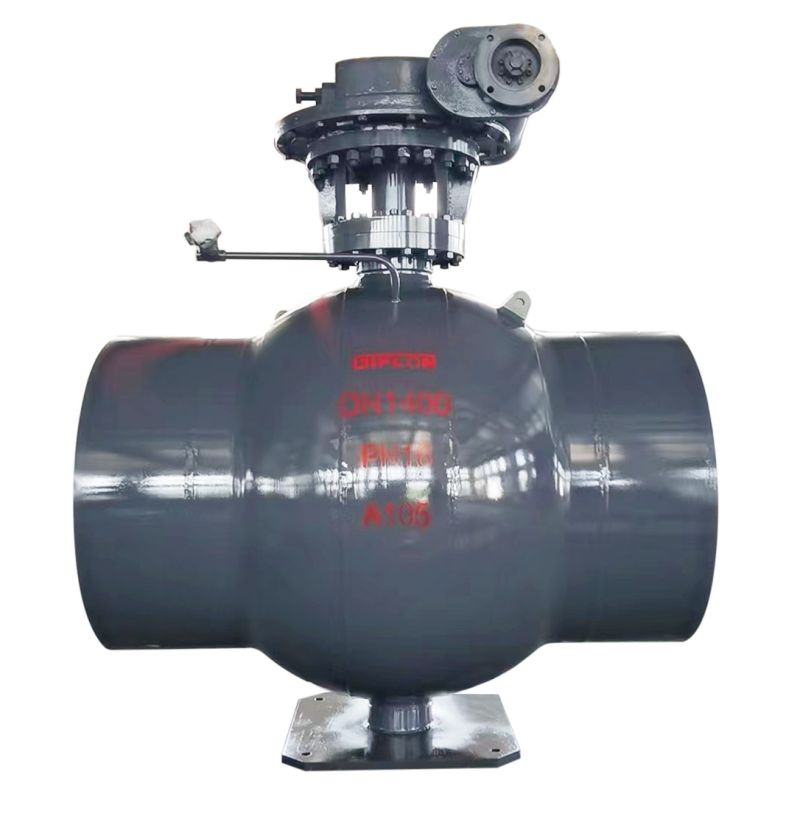
Discover the Latest Advancements in Globe Valves from China – All You Need to Know

By:Admin on 2023-11-30 09:22:20

Title: China's Advanced Globe Valve Technology Revolutionizes Industrial ApplicationsIntroduction:The Chinese Globe Valve (brand name removed) has unveiled its latest innovation in valve technology, revolutionizing the industrial sector with its cutting-edge design and exceptional performance capabilities. With its reliable and efficient operation, this breakthrough product is set to enhance productivity, reduce downtime, and elevate safety standards across various industries.Overview of the Globe Valve:The Globe Valve combines state-of-the-art engineering with meticulous craftsmanship to deliver a high-level performance in controlling the flow of fluid or gas within pipelines. The valve's unique design includes a spherical body and a movable disk, which together regulate the flow as required by the application. The precise control, durability, and versatility of this valve make it suitable for a wide range of industries, including oil and gas, chemical, power generation, and water treatment.Enhanced Features:The newly introduced Globe Valve exhibits several remarkable features that set it apart from its competitors. One remarkable attribute is its exceptional sealing mechanism, preventing any leakage and ensuring a completely sealed system. The valve's tight sealing capabilities maximize operational efficiency and prevent product loss, thereby reducing costs and minimizing environmental impact.Furthermore, the Globe Valve's advanced construction materials contribute to its robustness and longevity. The use of high-quality materials, such as corrosion-resistant alloys and durable seals, significantly extends the valve's lifespan, reducing maintenance needs and downtime while providing exceptional resistance against harsh operating conditions.Innovative Design for Optimal Performance:The engineers at (company name) have devoted endless hours to designing a Globe Valve that optimizes performance and provides reliable operation. Through in-depth research and development, they have successfully constructed a valve with unparalleled flow control capabilities. The valve's intelligent design ensures precise regulation of the medium's flow rate, thus offering enhanced efficiency and accuracy throughout the system.Moreover, the Globe Valve incorporates cutting-edge technology, such as pneumatic or electric actuators, which provide seamless automation to industrial processes. This automation feature enables efficient remote control and monitoring of the valve's operation, allowing industries to streamline their processes and maximize productivity.Applications and Benefits:The Chinese Globe Valve finds extensive application in numerous industries, showcasing its versatile adaptability to various industrial settings. In the oil and gas industry, it ensures the smooth transmission of oil and gas through pipelines, playing a crucial role in the safe transportation of valuable resources. Additionally, the valve's superior sealing technology guarantees optimal containment of hazardous chemicals in the chemical sector, prioritizing workforce safety.Furthermore, in power generation facilities, the Globe Valve contributes to the efficient regulation of steam flow, maintaining stable operations and enhancing energy production. Similarly, in water treatment plants, this valve offers precise control over water flow, ensuring the filtration and distribution processes operate seamlessly.The implementation of the Globe Valve in these diverse industries brings several benefits. By minimizing leakages and providing reliable operation, industrial facilities experience increased productivity, reduced downtime, and enhanced safety measures. The automation capabilities of the valve not only improve process efficiency but also reduce human error, consequently boosting overall operational performance.Conclusion:With its advanced technology, durable construction, and precise control capabilities, the Chinese Globe Valve is an outstanding example of China's excellence in industrial engineering. As this innovation continues to gain recognition globally, industries worldwide are benefiting from the improved safety, enhanced productivity, and operational efficiency brought about by this remarkable product. The Globe Valve stands as a testament to China's commitment to delivering high-quality engineering solutions that meet the demands of a rapidly advancing industrial landscape.

Read More

Exploring the Benefits of Large Size Sewage Gate Valves for Effective Wastewater Management

By:Admin on 2023-11-30 09:21:56

Title: Cutting-Edge Large Size Sewage Gate Valve Helps Revolutionize Wastewater ManagementIntroduction:In an exciting development for the wastewater management industry, a leading global valve manufacturer has unveiled a groundbreaking Large Size Sewage Gate Valve. Designed to improve the efficiency and reliability of wastewater systems, this advanced valve promises to revolutionize the way sewage is managed and treated. By addressing the unique challenges associated with handling large-scale sewage flow, this innovative solution is set to make a significant impact in creating cleaner and more sustainable communities.Body:Paragraph 1:The newly launched Large Size Sewage Gate Valve, crafted by a renowned valve manufacturer, represents a significant leap forward in wastewater management technology. With a focus on enhancing efficiency and minimizing environmental impact, this valve has been meticulously designed to meet the demanding requirements of large-scale sewage systems.Paragraph 2:One of the key features that sets this valve apart from its predecessors is its ability to handle high volumes of sewage without compromising performance. With a superior flow capacity, it ensures a seamless operation even under extreme pressure conditions. This robust construction is the result of cutting-edge engineering techniques and materials, which allow for efficient and reliable performance.Paragraph 3:In addition to its impressive flow capacity, the Large Size Sewage Gate Valve also boasts exceptional corrosion resistance. Constructed from specially selected materials, this valve effectively withstands the harsh operating conditions commonly found in sewage systems. By mitigating the risk of corrosion, it minimizes maintenance requirements and prolongs the lifespan of the valve, ultimately reducing operational costs.Paragraph 4:Furthermore, the implementation of a user-friendly design ensures easy installation and maintenance. The valve's intuitive interface allows for quick and hassle-free adjustments, contributing to the overall efficiency of the sewage system. With simplified maintenance procedures, operators can allocate more time and resources toward optimizing sewage treatment processes, resulting in a significant improvement in overall system performance.Paragraph 5:A notable advantage of the Large Size Sewage Gate Valve is its advanced control system, which allows for precise management of flow rates. This feature proves invaluable in preventing excessive or insufficient sewage flow, ensuring the optimal utilization of treatment facilities. By maintaining the appropriate flow rates, the valve aids in preventing overloads and blockages, leading to smoother operations and a reduced risk of system failure.Paragraph 6:The Large Size Sewage Gate Valve also prioritizes safety and environmental sustainability. Equipped with enhanced safety mechanisms, such as fail-safe shut-off capabilities, it mitigates the risk of wastewater spills and contamination. Additionally, this valve incorporates state-of-the-art sealing technologies to prevent leakage, thereby safeguarding the local ecosystem and public health.Paragraph 7:With growing concerns about the environmental impact of wastewater treatment, the Large Size Sewage Gate Valve offers a promising solution. Its innovative design reduces energy consumption by optimizing hydraulic conditions, thereby minimizing carbon emissions and promoting sustainability. By embracing this advanced technology, cities and municipalities can make significant strides in their efforts to create cleaner and healthier environments.Conclusion:The introduction of the Large Size Sewage Gate Valve marks a significant milestone in wastewater management. By combining cutting-edge engineering, reliability, and sustainability, this valve promises to revolutionize the industry. Through its superior flow capacity, corrosion resistance, ease of use, precise control, safety features, and environmental consciousness, this innovative valve will undoubtedly play a crucial role in improving wastewater treatment processes worldwide.

Read More

Discover the Latest Innovative Valve Technology for Optimal Performance

By:Admin on 2023-11-30 09:21:40

Title: Revolutionary NRV Valve: Transforming Industries with Cutting-Edge InnovationIntroduction:In an era where technological advancements are revolutionizing every industry, OEM NRV Valve emerges as a powerful player, integrating innovative solutions with unparalleled expertise. With a diverse range of applications, OEM NRV Valve is poised to transform industries around the globe. By combining cutting-edge technology, company expertise, and a commitment to excellence, OEM NRV Valve is pushing boundaries and reshaping the future.Cutting-Edge Technology Driving Innovation:OEM NRV Valve is at the forefront of engineering excellence, boasting a strong R&D team that continuously explores and applies new technologies. The company's commitment to innovation is evident in its groundbreaking NRV Valve, which stands for Non-Return Valve. This valve offers superior performance, robust construction, and efficient functionality, empowering various industries to overcome operational challenges effectively.The NRV Valve acts as a crucial safety component, preventing the reverse flow of fluids or gases, thereby protecting vital infrastructure and ensuring optimal operations. With advancements in material sciences, OEM NRV Valve has developed valves that can withstand extreme conditions, including high temperatures, corrosive environments, and intense pressure, making them suitable for a wide range of industrial applications.Revolutionizing Industries:The transformative power of OEM NRV Valve is felt across multiple industries, with their valves being adopted in energy production, oil and gas exploration, wastewater treatment, chemical processing, and many other critical sectors.In the energy sector, OEM NRV Valve's cutting-edge valves are utilized in power plants, ensuring efficient and safe steam management, preventing backflow, and minimizing energy loss. In the oil and gas industry, these valves play a pivotal role in wellhead operations, preventing hazardous gas blowbacks, and protecting personnel and infrastructure. The wastewater treatment plants utilize OEM NRV Valve's valves to regulate the flow of liquids and control backflow, reducing downtime and ensuring efficient treatment processes.Moreover, the chemical processing industry benefits greatly from OEM NRV Valve's products. These valves help in maintaining appropriate pressure levels, preventing contamination, and safeguarding personnel and equipment. Additionally, OEM NRV Valve's valves are becoming increasingly popular in the food and beverage industry, and pharmaceutical manufacturing, ensuring hygienic operations and preventing cross-contamination.Company Expertise and Commitment to Excellence:OEM NRV Valve's success can be attributed to its comprehensive understanding of industry demands and its commitment to delivering exceptional quality. The company employs highly skilled engineers, guided by industry experts, who work closely with clients to offer customized valve solutions tailored to specific requirements.By leveraging state-of-the-art manufacturing processes and technologies, coupled with rigorous quality control measures, OEM NRV Valve consistently delivers products that meet the highest industry standards. The company's commitment to excellence is further demonstrated through certifications such as ISO 9001 and API 6D, which signify its adherence to stringent quality management practices.Looking Towards the Future:As industries continue to evolve and demand advanced solutions, OEM NRV Valve remains at the forefront of innovation. The company's ongoing research and development initiatives aim to further enhance their valve capabilities, ensuring improved efficiency, durability, and safety. Furthermore, OEM NRV Valve is exploring opportunities to integrate digital technologies, such as IoT connectivity and smart monitoring systems, to enable real-time valve performance tracking and predictive maintenance.With a customer-centric approach and a dedication to technological advancement, OEM NRV Valve is poised to shape the future of industries globally. Their transformative NRV Valve continues to go above and beyond, ensuring reliable operations and safeguarding critical infrastructure.Conclusion:OEM NRV Valve's cutting-edge solutions and unwavering commitment to provide exceptional quality have positioned them as a leader in the valve manufacturing industry. With their revolutionary NRV Valve, the company is revolutionizing multiple industries, enabling efficient operations while ensuring the safety of personnel and infrastructure. As they continue to invest in research and development, OEM NRV Valve is set to further redefine industry expectations and push the boundaries of innovation.

Read More