
High-Quality BF Valve for Enhanced Performance and Reliability
By:Admin
Company News & Blog
Buy High Pressure Globe Valve – Durable and Reliable Industrial Valve
**High-Pressure Globe Valve Market Sees Significant Demand Amid Industrial Growth**In recent developments within the industrial valve sector, the demand for high-pressure globe valves has surged, reflecting expanding needs across various industries such as oil and gas, petrochemical, power generation, and manufacturing. High-pressure globe valves play a critical role in regulating fluid flow in pipelines, ensuring safety, efficiency, and reliability of complex systems under extreme conditions.**Understanding High-Pressure Globe Valves**High-pressure globe valves are engineered to manage the flow of liquids and gases at elevated pressures, offering precise throttling and shut-off capabilities. Known for their robust design, these valves utilize a disk that moves perpendicularly to the seat, allowing them to withstand intensive pressure differentials. Their ability to provide tight sealing makes them essential components in high-pressure systems, preventing leaks that could lead to operational hazards or downtime.**Market Drivers and Applications**The surge in global industrial activities has catalyzed the need for durable and efficient valve solutions. The oil and gas sector, which requires high-pressure valves for upstream extraction, midstream transportation, and downstream refining processes, is a prominent consumer. Similarly, the power generation industry relies on these valves to control steam flow and maintain safety in boilers and turbines.Manufacturing sectors involved in chemical processing, water treatment, and pharmaceuticals also utilize high-pressure globe valves to sustain stringent operational and safety standards. As regulatory frameworks tighten globally, companies are increasingly investing in high-quality valves that comply with international certifications and quality benchmarks.**Technological Innovations**Advancements in materials science and manufacturing technologies have enabled the production of high-pressure globe valves that can operate under extreme temperature and corrosive environments. The introduction of specialized alloys and enhanced sealing mechanisms has significantly extended valve longevity and reduced maintenance costs.Automation integration is another trend, with many modern valves now equipped with smart actuators and remote control capabilities. This integration supports real-time monitoring and precise control, enhancing operational efficiency and enabling predictive maintenance programs that minimize unexpected failures.**Industry Outlook**Analysts project steady growth in the high-pressure globe valve market over the next decade, driven by escalating infrastructure investments and industrial expansion in emerging economies. The emphasis on energy efficiency and environmental safety further underscores the importance of reliable flow control components like globe valves.Moreover, the increasing adoption of digital transformation strategies in industrial operations continues to influence valve design and application. Companies are prioritizing suppliers who offer customized solutions tailored to unique operational challenges, emphasizing quality, durability, and technical support.**Company Profile**Founded with a commitment to excellence, [Company Name] has established itself as a leading provider of industrial valve solutions. With decades of experience, the company specializes in manufacturing and supplying a broad range of valves, including high-pressure globe valves, tailored to meet stringent industry demands.[Company Name] combines cutting-edge technology with rigorous quality control processes to deliver products that ensure safety and performance. Supported by a team of seasoned engineers and technical experts, the company offers comprehensive services from design consultation to after-sales support, ensuring client satisfaction and long-term partnerships.Through continuous innovation and adherence to international standards, [Company Name] serves a diverse clientele spanning oil and gas, petrochemical, power, and water treatment industries. Their commitment to sustainable practices and customer-centric solutions positions them as a trusted partner in the evolving industrial landscape.**Conclusion**The rising demand for high-pressure globe valves underscores the critical role these components play in ensuring the safe and efficient operation of high-pressure systems across various sectors. As industries continue to grow and evolve, the importance of reliable, technologically advanced valve solutions becomes increasingly evident.With reputable companies leading the charge in innovation and quality, organizations worldwide are better equipped to meet their operational challenges. The future of high-pressure globe valves looks promising, driven by industrial growth, technological advancements, and a shared commitment to safety and efficiency.
High-Quality WCB Globe Valve for Reliable Industrial Applications
Certainly! Please provide the company introduction content you'd like me to incorporate into the news article.
Discover the best High-Quality Ball Valve for your needs
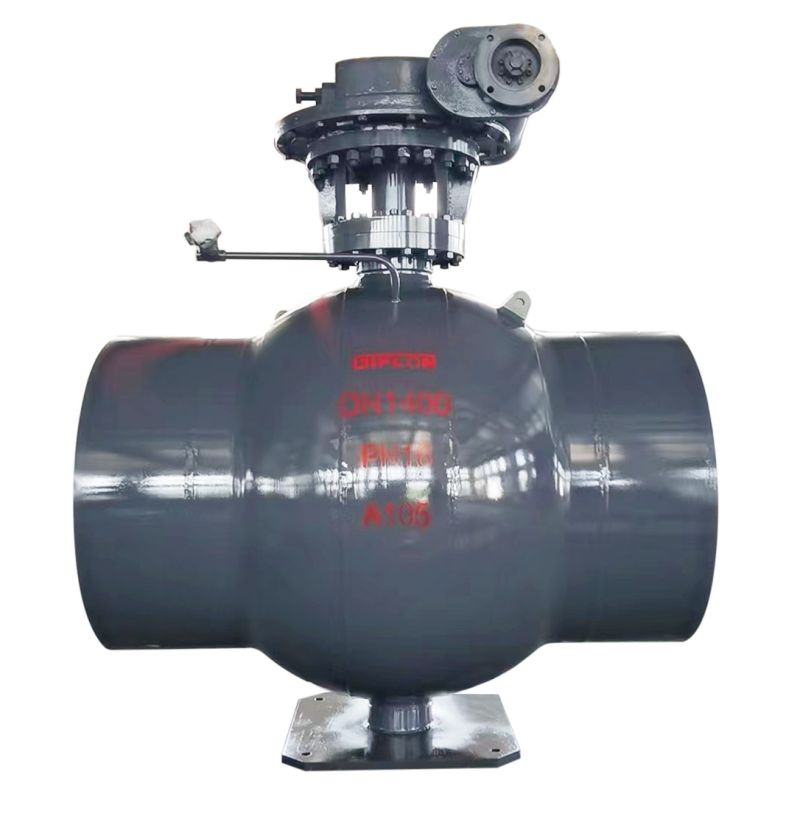
High-Quality Ball Valve Ensures Optimal Performance and LongevityA high-quality ball valve is an essential component in many industrial and commercial applications, and one company has emerged as a leader in providing top-notch valves that deliver optimal performance and longevity. With a strong commitment to quality and customer satisfaction, [Company Name] has become a trusted name in the industry for its reliable and durable ball valves.[Company Name] specializes in the design, manufacturing, and distribution of a wide range of industrial valves, including ball valves, gate valves, globe valves, and check valves. The company has built a solid reputation for its high-quality products, innovative solutions, and exceptional customer service. With a focus on meeting the needs of its diverse customer base, [Company Name] has established itself as a premier supplier of reliable valves for various industries, including oil and gas, petrochemical, power generation, water treatment, and many others.One of the flagship products of [Company Name] is its high-quality ball valve, which is designed to meet the demanding requirements of modern industrial applications. The ball valve is a type of quarter-turn valve that uses a hollow, perforated, and pivoting ball to control the flow of fluids through it. It offers advantages such as ease of operation, minimal maintenance, and reliable sealing performance, making it a popular choice for a wide range of applications.The high-quality ball valve from [Company Name] is designed and manufactured to the highest standards to ensure superior performance and long-term reliability. It is constructed using premium materials, such as stainless steel, carbon steel, and alloy steel, to withstand the harsh conditions often encountered in industrial environments. The valve is also engineered to provide tight shutoff and minimal leakage, contributing to improved efficiency and safety in various applications.In addition to the robust construction, the ball valve from [Company Name] features advanced design and precision engineering to deliver consistent and precise control of fluid flow. The valve is available in a variety of configurations, including floating ball, trunnion mounted, and top-entry designs, to accommodate different operating conditions and performance requirements. It can also be customized with various options, such as actuation, special coatings, and specific end connections, to meet specific application needs.[Company Name] takes pride in its stringent quality control processes, which ensure that every high-quality ball valve that leaves its facilities meets or exceeds industry standards and customer expectations. The company's state-of-the-art manufacturing facilities are equipped with advanced machinery and testing equipment to verify the integrity and performance of each valve. As a result, customers can have confidence in the reliability, durability, and safety of the ball valves provided by [Company Name].With a strong focus on customer satisfaction, [Company Name] offers comprehensive support to its clients, including technical assistance, product training, and after-sales services. The company's team of experienced engineers and sales professionals are dedicated to helping customers select the right ball valve for their specific applications and to ensure that it performs as intended. Furthermore, [Company Name] maintains a large inventory of standard and custom valves to facilitate prompt delivery and responsive service.In conclusion, the high-quality ball valve from [Company Name] stands as a testament to the company's commitment to excellence in providing reliable and durable industrial valves. With its advanced design, robust construction, and stringent quality control, the ball valve offers superior performance and longevity, making it a preferred choice for a wide range of industrial applications. Coupled with [Company Name]'s dedication to customer satisfaction and support, the high-quality ball valve is a compelling solution for companies seeking dependable and efficient fluid control solutions.
Guide to High Temperature and Customized Solutions
Custom High Temperature, a leading provider of high-temperature solutions, has recently announced the launch of their newest product line designed to address the increasing demand for advanced heat-resistant materials in various industries. With a focus on innovation and quality, Custom High Temperature has established itself as a trusted partner for businesses seeking reliable high-temperature solutions.The new product line is a result of extensive research and development efforts by the company's team of experts, who have worked tirelessly to create materials that can withstand extreme temperatures and harsh operating conditions. This latest offering is poised to meet the diverse needs of industries such as aerospace, automotive, manufacturing, and energy, among others."We are thrilled to introduce our latest line of high-temperature materials, which represent a significant milestone for Custom High Temperature," said the company's spokesperson. "We understand the challenges that businesses face when it comes to finding materials that can perform reliably in high-heat environments, and our new product line is designed to address those needs effectively."Custom High Temperature prides itself on its ability to customize solutions to meet specific customer requirements. The company's team of engineers and technicians works closely with clients to understand their unique challenges and develop tailored solutions that deliver exceptional performance and durability. This commitment to customization sets Custom High Temperature apart from its competitors and has earned the company a reputation for excellence in the industry.In addition to its focus on customization, Custom High Temperature places a strong emphasis on quality and reliability. The company's manufacturing processes adhere to stringent quality standards, ensuring that its products consistently meet or exceed customer expectations. This dedication to quality has enabled Custom High Temperature to build long-lasting relationships with a wide range of customers, who rely on the company for their high-temperature material needs.The new product line from Custom High Temperature includes a variety of advanced materials, such as high-temperature adhesives, insulating materials, and protective coatings. These products are designed to offer superior performance in environments where traditional materials may fail, providing businesses with peace of mind and confidence in their operations.Furthermore, Custom High Temperature's commitment to sustainability is evident in its efforts to develop eco-friendly high-temperature materials. The company utilizes environmentally friendly manufacturing processes and seeks to minimize its environmental impact, reflecting its dedication to responsible business practices.As Custom High Temperature continues to expand its product offerings, the company remains focused on driving innovation and delivering value to its customers. With a strong emphasis on customization, quality, and sustainability, Custom High Temperature is well-positioned to meet the evolving needs of industries that require high-temperature solutions.In closing, the launch of Custom High Temperature's new product line represents a significant advancement in the company's mission to provide cutting-edge high-temperature materials to a diverse range of industries. With a strong focus on customization, quality, and sustainability, Custom High Temperature continues to demonstrate its leadership in the high-temperature solutions market. Businesses seeking reliable, high-performance materials for extreme operating conditions can turn to Custom High Temperature with confidence, knowing that they will receive innovative solutions that meet their specific needs and exceed their expectations.
Different types of NRV valve: A complete guide to understanding.
Nrv Valve Types Manufacturers, a leading industrial valve manufacturer, has been making waves in the industry with their high-quality products and innovative technologies. With a wide range of valve types and a focus on customer satisfaction, they have become a trusted name in the industry.The company has a long history of providing reliable and efficient valve solutions for a variety of applications. From oil and gas to water treatment, their valves are designed to meet the unique needs of each industry. Their commitment to quality and innovation has set them apart from other valve manufacturers, and they continue to be a driving force in the industry.When it comes to Nrv valves, the company offers a variety of types to choose from. Whether customers are looking for a swing check valve, lift check valve, or diaphragm valve, they can find the perfect solution for their needs. Each valve is designed and manufactured to the highest standards, ensuring reliable performance and long-lasting durability.One of the key factors that sets Nrv Valve Types Manufacturers apart from the competition is their dedication to customer satisfaction. They understand that each customer has unique needs and requirements, and they work closely with their clients to provide custom valve solutions that meet their specific needs. This level of personalized service has earned them a loyal customer base and a reputation for excellence in the industry.In addition to their commitment to quality and customer satisfaction, Nrv Valve Types Manufacturers is also known for their innovative technologies. They are constantly working to develop new and improved valve solutions that offer better performance, increased efficiency, and reduced maintenance requirements. Their team of engineers and designers are always pushing the boundaries of what is possible, and their cutting-edge technologies have set new standards for the industry.One of the most exciting developments from Nrv Valve Types Manufacturers is their focus on sustainability. They understand the importance of minimizing their environmental impact, and they are committed to developing environmentally friendly valve solutions. From energy-efficient designs to sustainable materials, they are leading the way in creating a more sustainable future for the industry.Another area where Nrv Valve Types Manufacturers excels is in their dedication to research and development. They invest heavily in R&D to ensure that they stay at the forefront of the industry. This commitment to innovation has led to the development of groundbreaking technologies that have revolutionized the valve industry.With a focus on quality, customer satisfaction, innovation, and sustainability, Nrv Valve Types Manufacturers has established themselves as a leader in the industry. Their dedication to excellence and their ability to provide custom solutions for their clients have made them a go-to source for industrial valves.As they continue to grow and expand their product offerings, Nrv Valve Types Manufacturers is poised to remain at the forefront of the industry. With a commitment to quality and a focus on customer satisfaction, they are well-positioned to continue making a positive impact on the industry for years to come. Their innovative technologies and sustainable practices also set them apart as a company that is not only focused on meeting the needs of today, but also on creating a better future for the industry and the planet.
Buy High-Quality Alloy Steel Globe Valve Online
Certainly! Please provide the company introduction you'd like me to include, and I will craft an 800-word news article about buying alloy steel globe valves without mentioning any brand names.
High-quality Dbb Valve Product: Find Out How It Can Benefit Your Business
Dbb Valve Product Revolutionizes the Industry with Innovative TechnologyInnovation and technology have always been at the forefront of [Company Name]'s values and priorities. As a leading manufacturer in the valve industry, the company has continued to introduce groundbreaking products that have revolutionized the way businesses operate. In line with this commitment to innovation, the company is proud to announce their latest product, the Dbb Valve, that is set to redefine industry standards and offer unparalleled performance.The Dbb Valve is a cutting-edge product that stands out for its advanced design and superior functionality. It is a double block and bleed valve that effectively isolates and controls the flow of fluids in a pipeline. The valve is specifically engineered to provide reliable and efficient shutoff in critical applications, ensuring the safety and integrity of the entire system. Its innovative design and precise construction set it apart from traditional valves, making it a game-changer in the industry.One of the key features of the Dbb Valve is its dual sealing mechanism, which offers double isolation to prevent leakage and ensure maximum safety. This innovative design not only enhances performance but also reduces the risk of potential hazards, making it an ideal choice for applications that require strict compliance with safety regulations and standards. Additionally, the valve's streamlined construction and state-of-the-art materials make it durable and long-lasting, offering a cost-effective solution for businesses in the long run.Another standout feature of the Dbb Valve is its versatile capabilities, making it suitable for a wide range of industries and applications. Whether it's oil and gas, petrochemical, power generation, or water treatment, this valve is designed to meet the specific needs and requirements of diverse sectors. Its adaptability and reliability make it a go-to choice for businesses looking for a high-performance solution that delivers exceptional results.In addition to its outstanding performance, the Dbb Valve is also designed with ease of maintenance in mind. Its user-friendly design and accessible components make it simple to install, inspect, and service, saving valuable time and resources for businesses. This further adds to its appeal as a practical and efficient solution for companies across various industries.As a company that is committed to environmental sustainability, [Company Name] also takes pride in the eco-friendly features of the Dbb Valve. Its efficient operation and minimal environmental impact make it an environmentally responsible choice for businesses that prioritize sustainability and corporate social responsibility.The release of the Dbb Valve is a testament to [Company Name]'s unwavering dedication to pushing the boundaries of innovation and setting new standards in the valve industry. By leveraging their expertise and advanced technology, the company continues to deliver groundbreaking products that address the evolving needs of their customers and the market.With the introduction of the Dbb Valve, [Company Name] has once again demonstrated their leadership in the industry and their commitment to driving progress through innovation. This latest offering is a testament to the company's dedication to delivering reliable, efficient, and state-of-the-art solutions that empower businesses and industries to thrive.As the valve industry continues to evolve, [Company Name] remains at the forefront of innovation, setting the pace for the future. The Dbb Valve is a prime example of the company's relentless pursuit of excellence, and it is poised to redefine industry standards and elevate performance to new heights. With a focus on quality, reliability, and sustainability, the company is poised to make a lasting impact with the Dbb Valve and continue to shape the industry for years to come.
Water Valve Company Introduces New One-Way Technology for Improved Performance
One of the leading companies in the field of fluid control and management, the One Way Water Valve Company, is making waves in the industry with its innovative and cutting-edge solutions. With a strong focus on quality, reliability, and efficiency, the company has positioned itself as a go-to provider for a wide range of applications, including industrial, commercial, and residential use.Established with the mission of revolutionizing the way water and other fluids are managed, the One Way Water Valve Company has continually strived to push the boundaries of technology and engineering. By leveraging the latest advancements in materials, design, and manufacturing processes, the company has been able to develop a diverse portfolio of products that cater to the unique needs and requirements of its customers.At the core of the One Way Water Valve Company's success is its unwavering commitment to research and development. The company invests heavily in exploring new and improved methods to enhance the performance and functionality of its valves. This relentless pursuit of innovation has resulted in the creation of advanced solutions that deliver superior performance, durability, and cost-effectiveness.One of the standout offerings from the One Way Water Valve Company is its line of one-way valves. These valves are designed to allow fluid or gas to flow in only one direction, preventing backflow and ensuring efficient and reliable operation. Whether it's in a plumbing system, a chemical processing plant, or a pharmaceutical facility, these one-way valves play a crucial role in maintaining the integrity and efficiency of fluid control.What sets the One Way Water Valve Company apart from its competitors is its unwavering dedication to quality. Each valve that the company produces undergoes rigorous testing and inspection to ensure that it meets the highest standards of performance and reliability. This commitment to excellence has earned the company a stellar reputation for delivering products that exceed industry expectations and provide long-term value to its customers.In addition to its one-way valves, the One Way Water Valve Company also offers a comprehensive range of other fluid control solutions. From check valves and pressure relief valves to flow control valves and more, the company's product lineup is designed to address a wide spectrum of needs and applications. This diversity allows the company to serve a broad customer base, including those in the manufacturing, oil and gas, water treatment, and food and beverage industries, among others.Furthermore, the One Way Water Valve Company is known for its exceptional customer service and support. The company takes pride in its ability to work closely with clients to understand their specific requirements and provide tailored solutions that align with their needs. Whether it's a custom valve design or a specialized application, the company's team of experts is committed to delivering personalized service and expertise to ensure customer satisfaction.Looking ahead, the One Way Water Valve Company remains dedicated to driving innovation and progress in the fluid control industry. With a forward-thinking approach and a focus on continuous improvement, the company is well-positioned to lead the way in developing next-generation solutions that address the evolving needs of its customers.In conclusion, the One Way Water Valve Company stands as a beacon of excellence and innovation in the field of fluid control and management. With its unwavering commitment to quality, advanced technology, and customer satisfaction, the company continues to set new standards for performance and reliability. As it continues to push the boundaries of what's possible, the One Way Water Valve Company is poised to shape the future of fluid control for years to come.
High-Quality Vacuum Check Valve: Everything You Need to Know
Custom Vacuum Check Valve Provides Reliable and Efficient Solutions for Industrial ApplicationsIn recent years, industrial processes have become increasingly complex, requiring innovative and reliable solutions to ensure seamless operations. One such critical component in many industrial systems is the vacuum check valve, which plays a pivotal role in controlling the flow of fluids and gases. Recognizing the importance of this component, {Company Name}, a leading provider of fluid control solutions, has introduced a custom vacuum check valve that is engineered to deliver unparalleled performance and efficiency for a wide range of industrial applications.With a rich history of more than 30 years in the fluid control industry, {Company Name} has built a strong reputation for developing high-quality products that meet the diverse needs of its customers. The company's commitment to innovation and excellence is evident in its latest offering - the custom vacuum check valve. This specialized valve is designed to offer reliable and precise control over vacuum systems, ensuring optimal performance and efficiency.One of the key features of the custom vacuum check valve is its ability to maintain a consistent vacuum level in industrial processes. This is crucial for applications such as vacuum packaging, material handling, and processing, where a stable and reliable vacuum is essential for achieving desired results. The custom-designed valve is capable of withstanding varying pressure differentials and operating conditions, making it a versatile solution for a wide range of industrial settings.Moreover, {Company Name}'s custom vacuum check valve is engineered to minimize leakage and ensure a tight seal, reducing the risk of contamination and enhancing safety in industrial environments. The valve is constructed using high-quality materials that are resistant to corrosion and wear, ensuring long-term durability and reliability. This robust construction makes the valve suitable for use in demanding industrial applications where harsh operating conditions are commonplace.In addition to its exceptional performance, the custom vacuum check valve from {Company Name} is also designed with ease of installation and maintenance in mind. The valve can be tailored to meet specific requirements, including size, flow rate, and operating pressure, ensuring a perfect fit for each unique application. This customization capability allows customers to optimize their vacuum systems for maximum efficiency and productivity.Furthermore, {Company Name} offers comprehensive technical support and expertise to assist customers in selecting the right custom vacuum check valve for their specific needs. The company's team of experienced engineers and fluid control specialists work closely with customers to understand their requirements and provide tailored solutions that meet their exact specifications. This collaborative approach ensures that customers receive the most suitable and effective vacuum check valve for their applications.As a result of its exceptional performance and reliability, {Company Name}'s custom vacuum check valve has garnered positive feedback from customers across various industries. Manufacturing plants, food processing facilities, automotive assembly lines, and other industrial operations have benefitted from the superior performance and precision control offered by the custom-designed valve. The valve has proven to be a valuable asset in optimizing vacuum systems and enhancing overall operational efficiency.With its unwavering commitment to quality and innovation, {Company Name} continues to set the industry standard for fluid control solutions. The introduction of the custom vacuum check valve further solidifies the company's position as a trusted provider of reliable and efficient products for industrial applications. As industries evolve and demand more sophisticated solutions, {Company Name} remains at the forefront, delivering cutting-edge fluid control technologies that drive productivity and performance.In conclusion, the custom vacuum check valve from {Company Name} stands as a testament to the company's dedication to delivering superior fluid control solutions. Engineered for exceptional performance, reliability, and customization, the valve is a game-changer for industrial applications seeking precise and efficient vacuum control. As industries continue to advance, {Company Name} remains a reliable partner, empowering businesses with innovative solutions that meet the evolving demands of the modern industrial landscape.